


How Aluminum Alloy Bell Housing Enhances the Durability of Packaging Materials
Release Time:
Oct 25,2025
How Aluminum Alloy Bell Housing Enhances the Durability of Packaging Materials Introduction In the world of packaging materials, the quest for durability and strength is never-ending. **Aluminum alloy bell housing** has emerged as a game-changer, providing an effective solution for various packaging needs. This article delves into how aluminum alloy bell housing enhances the durability of packagin
How Aluminum Alloy Bell Housing Enhances the Durability of Packaging Materials
Introduction
In the world of packaging materials, the quest for durability and strength is never-ending. **Aluminum alloy bell housing** has emerged as a game-changer, providing an effective solution for various packaging needs. This article delves into how aluminum alloy bell housing enhances the durability of packaging materials, examining its properties, benefits, and applications across different industries.
Table of Contents
1. Understanding Aluminum Alloys
2. The Role of Bell Housing in Packaging
3. Benefits of Aluminum Alloy in Packaging Durability
3.1 Lightweight Nature
3.2 Corrosion Resistance
3.3 Thermal Conductivity
4. Applications of Aluminum Alloy Bell Housing in Packaging
4.1 Food and Beverage Packaging
4.2 Pharmaceutical Packaging
4.3 Electronics and Components Packaging
5. Case Studies: Success Stories Using Aluminum Alloy Bell Housing
6. FAQs about Aluminum Alloy Bell Housing in Packaging
7. Conclusion
1. Understanding Aluminum Alloys
Aluminum alloys are materials made from aluminum combined with other elements to enhance their properties. These alloys can be categorized into two main types: wrought and cast. Wrought alloys are typically used in products requiring high strength, while cast alloys are ideal for applications that demand complex shapes.
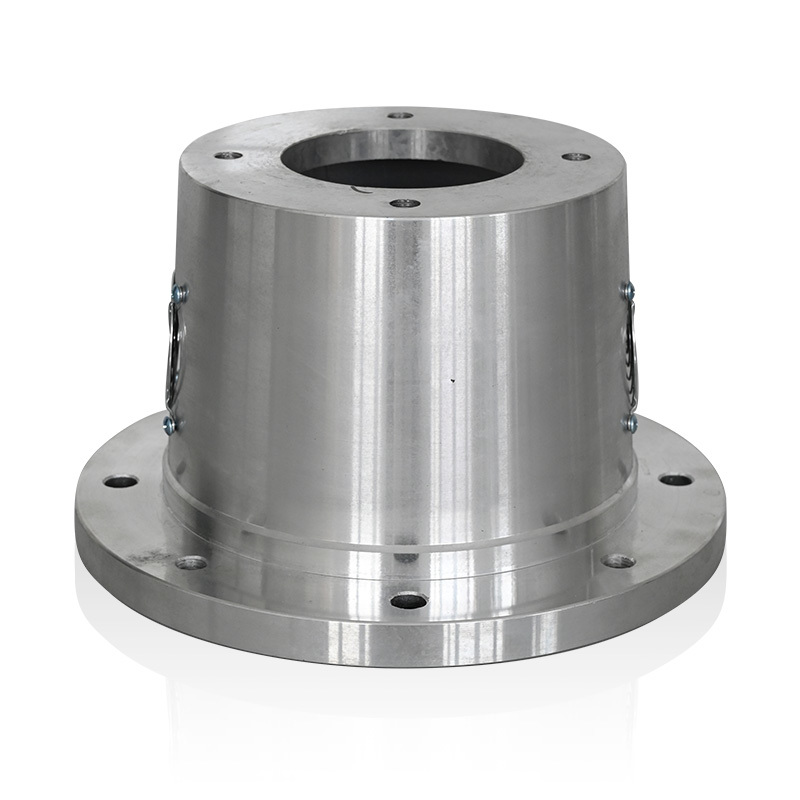
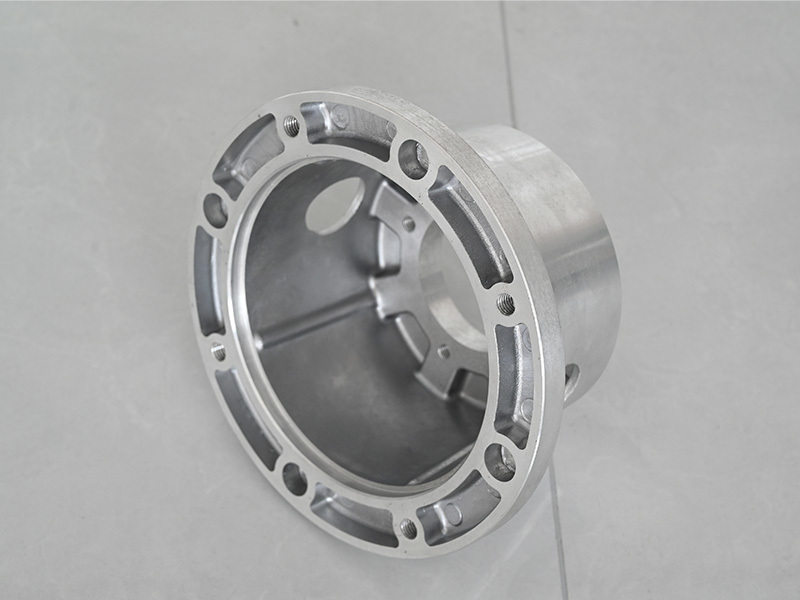
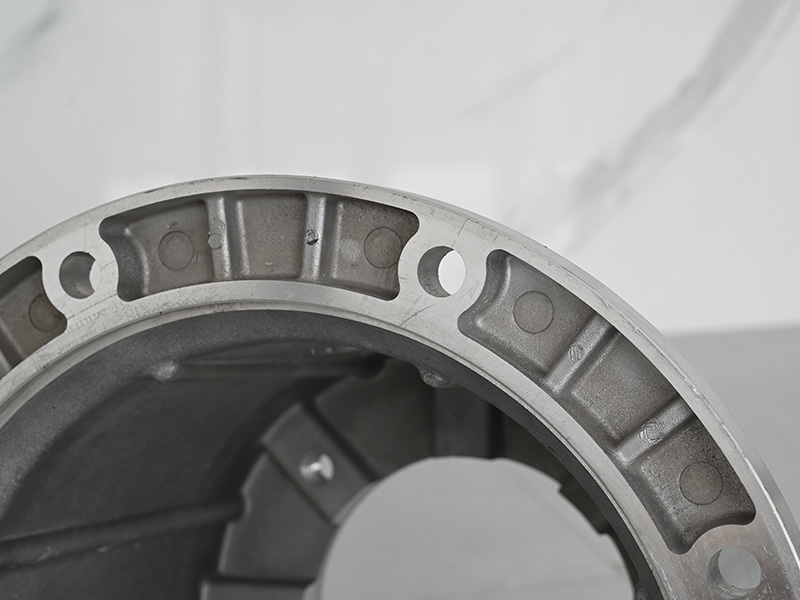
**Aluminum alloy bell housing** refers to a particular application where these alloys form a protective casing, often for mechanical components. They are renowned for their robustness, making them an excellent choice for packaging materials.
2. The Role of Bell Housing in Packaging
Bell housing serves as a protective barrier in various packaging applications. By encasing delicate items, it prevents damage during transportation and handling. The use of **aluminum alloys** in bell housing enhances strength and performance, ensuring packages withstand the rigors of shipping and storage.
Bell housing made from aluminum alloys offers **additional benefits** such as customization and flexibility in design, which allows for tailored solutions to meet specific packaging requirements.
3. Benefits of Aluminum Alloy in Packaging Durability
Aluminum alloys provide numerous advantages when utilized in packaging, especially concerning durability.
3.1 Lightweight Nature
One of the standout features of aluminum alloys is their lightweight nature. This attribute not only helps reduce shipping costs but also makes handling easier. Despite their lightness, aluminum alloys maintain exceptional strength, making them ideal for protective housing.
3.2 Corrosion Resistance
Aluminum inherently possesses excellent corrosion resistance due to the formation of a protective oxide layer. This characteristic is crucial for packaging materials, especially in industries where exposure to moisture or chemicals is prevalent. The resilience of aluminum alloy bell housing ensures that products remain safe from corrosion-related damage, extending the shelf life of packaged goods.
3.3 Thermal Conductivity
**Thermal conductivity** is another significant benefit of aluminum alloys. Their ability to dissipate heat efficiently minimizes the risk of heat-related damage to sensitive products. In industries like food and pharmaceuticals, maintaining the appropriate temperature is vital, making aluminum alloy bell housing a strategic choice for packaging.
4. Applications of Aluminum Alloy Bell Housing in Packaging
Aluminum alloy bell housing finds applications across various sectors, demonstrating its versatility in packaging solutions.
4.1 Food and Beverage Packaging
In the food and beverage industry, packaging integrity is paramount. Aluminum alloy bell housing helps maintain product freshness while protecting against external contaminants. Its lightweight yet strong properties contribute to safer transportation, which is crucial for perishable goods.
4.2 Pharmaceutical Packaging
The pharmaceutical sector demands strict adherence to safety and quality standards. Aluminum alloy bell housing provides an effective barrier against contamination, ensuring medications remain uncontaminated. Moreover, its ability to withstand extreme temperatures makes it suitable for sensitive pharmaceutical products.
4.3 Electronics and Components Packaging
In electronics, the packaging must safeguard delicate components against physical damage and static electricity. Aluminum alloy bell housing is effective in protecting these components. Its robust structure offers a shield against shocks, ensuring the safe transport of valuable electronics.
5. Case Studies: Success Stories Using Aluminum Alloy Bell Housing
Numerous companies have successfully implemented aluminum alloy bell housing in their packaging strategies. For instance, a leading beverage company adopted aluminum alloy bell housing to enhance its product packaging. The result was a significant reduction in breakage during transit, leading to increased customer satisfaction and reduced costs related to damaged goods.
Similarly, a pharmaceutical firm reported improved compliance with safety regulations after switching to aluminum alloy bell housing for its medication packaging. The durability and protection offered by aluminum alloys helped ensure the integrity of their products throughout the supply chain.
6. FAQs about Aluminum Alloy Bell Housing in Packaging
**Q1: What is aluminum alloy bell housing?**
A1: Aluminum alloy bell housing is a protective casing made from aluminum alloys, providing durability and strength for various packaging applications.
**Q2: Why is aluminum preferred for packaging materials?**
A2: Aluminum is lightweight, corrosion-resistant, and thermally conductive, making it an ideal choice for packaging materials across various industries.
**Q3: Can aluminum alloy bell housing be customized for specific needs?**
A3: Yes, aluminum alloy bell housing can be customized to fit specific product dimensions and packaging requirements.
**Q4: How does aluminum alloy bell housing contribute to sustainability?**
A4: Aluminum is recyclable and can be reused, contributing to sustainable packaging solutions and reducing environmental impact.
**Q5: What industries benefit the most from aluminum alloy bell housing?**
A5: Industries such as food and beverage, pharmaceuticals, and electronics significantly benefit from aluminum alloy bell housing due to its protective qualities.
7. Conclusion
The utilization of **aluminum alloy bell housing** in packaging materials represents a remarkable advancement in durability and protection. Its lightweight nature, corrosion resistance, and thermal conductivity make it an invaluable asset across various industries. As we move toward more sustainable practices, aluminum alloy bell housing continues to prove itself as a reliable choice for enhancing the durability of packaging materials. Investing in this innovative solution not only safeguards products but also optimizes packaging processes, ultimately leading to greater efficiency and customer satisfaction.
Keywords:
You Can Also Learn More About Industry Trends


Specializing In The Research And Development And Sales Of Hydraulic Products


Contact Us
Phone/Whatsapp
+8613933722213 / +8613933744887
Address
No. 158, Xiaotun Automobile and Motorcycle Industrial Zone, Qinghe County, Hebei Province